Process Analytical Technology : The Future of Quality Assurance in Pharmaceutical Manufacturing
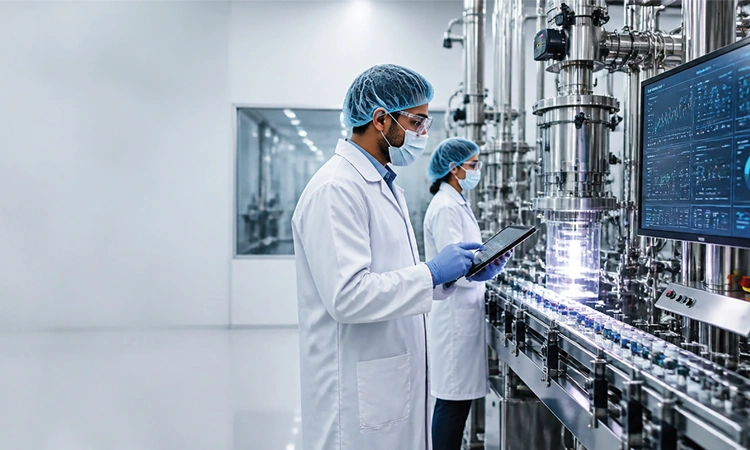
The pharmaceutical industry operates in an environment where quality, safety and consistency are non-negotiable. Every tablet, capsule, injectable or biologic must meet stringent specifications before it reaches the patient. Traditionally, quality assurance has relied heavily on laboratory testing of samples taken from manufacturing batches. While effective, this approach provides information primarily after a process has taken place.
Process Analytical Technology (PAT) is transforming this model. By using real-time measurement, process monitoring, advanced sensors, data analytics and automation, PAT enables manufacturers to understand and control pharmaceutical processes as they occur. Instead of simply testing quality into the finished product, PAT supports a more proactive philosophy-building quality into the process itself.
From End-Product Testing to Real-Time Quality
Traditional pharmaceutical manufacturing typically involves sampling materials at various stages and sending them to a laboratory for analysis. Results may take minutes or hours, and in some cases longer. If a problem is detected, a significant quantity of material may already have been processed.
PAT changes this approach by continuously monitoring critical process and product parameters. Information generated during manufacturing can be used to determine whether the process remains within its desired operating range.
The objective is not necessarily to eliminate conventional laboratory testing, but to complement it with timely process information. This enables manufacturers to identify deviations earlier and make appropriate adjustments before they result in rejected batches.
What is Process Analytical Technology?
PAT can be broadly defined as a system for designing, analysing and controlling manufacturing processes through timely measurements of critical quality and performance attributes.
A PAT framework can incorporate sensors, analytical instruments, process-control systems, data-management platforms and statistical or computational tools.
Depending on the process, manufacturers can monitor parameters such as temperature, pressure, pH, moisture, particle size, concentration, chemical composition and blend uniformity.
Technologies such as near-infrared (NIR) spectroscopy, Raman spectroscopy, ultraviolet-visible spectroscopy, chromatography, particle-size analysis and imaging can provide valuable information without necessarily removing material from the production line.
![Real Time Monitoring]() Real-Time Monitoring
 Real-Time Monitoring
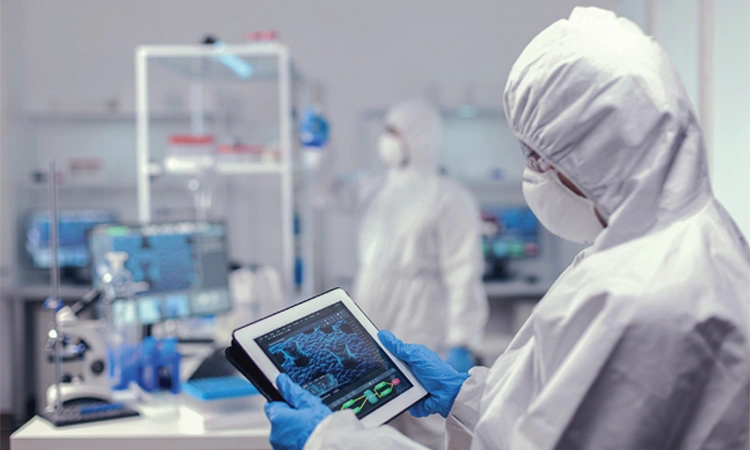
One of PAT’s greatest advantages is the ability to monitor processes continuously or at very short intervals.
Consider a pharmaceutical blending operation. Uniform distribution of active pharmaceutical ingredients (APIs) is essential to ensure that every dosage unit contains the intended amount. Conventional sampling provides information about selected locations and times. In-line or at-line analytical technologies can provide a much broader understanding of blend behaviour.
Similarly, during drying, real-time moisture measurement can help determine when the material has reached the required condition. Rather than relying solely on predetermined drying times, manufacturers can make decisions based on actual process performance.
This can improve consistency while potentially reducing over-processing.
Enabling Quality by Design
PAT is closely associated with the broader Quality by Design (QbD) philosophy. QbD seeks to understand how raw materials, process parameters and manufacturing conditions influence final product quality.
This requires identifying critical quality attributes (CQAs) and critical process parameters (CPPs). PAT provides the measurement capability required to monitor these factors and establish relationships between process conditions and product quality.
The result is a more scientific approach to manufacturing. Instead of simply determining whether the finished product passes or fails a specification, manufacturers can develop a deeper understanding of why the product achieves its desired characteristics.
Reducing Variability and Waste
Manufacturing variability can arise from raw materials, equipment, environmental conditions and process parameters. Even small variations can sometimes affect pharmaceutical quality.
Continuous process monitoring can identify trends before they develop into significant deviations. Corrective action can then be taken at an earlier stage.
This can reduce rejected batches, reprocessing, material wastage and unnecessary consumption of energy and utilities. PAT can therefore deliver benefits beyond quality assurance by contributing to operational efficiency and sustainability.
![PAT and Automation]() PAT and Automation
 PAT and Automation
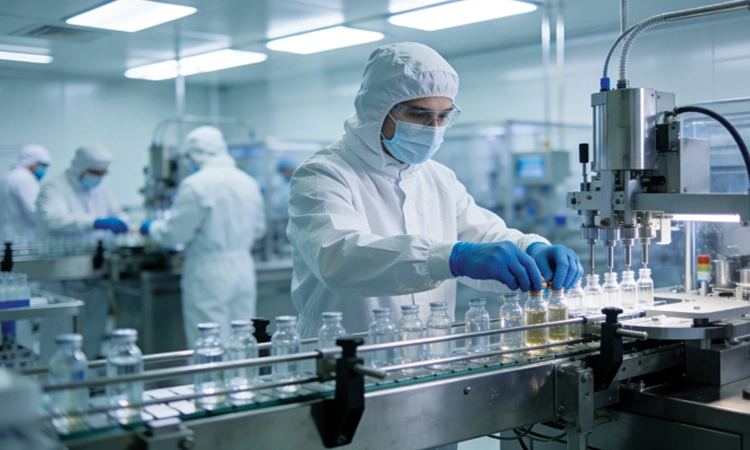
The effectiveness of PAT increases significantly when analytical information is integrated with automated process-control systems.
A sensor may identify that a process parameter is moving outside its desired range. The control system can then automatically adjust a suitable operating variable or alert the operator.
This creates a closed-loop approach in which measurement, analysis and control work together.
Modern manufacturing systems can integrate PAT data with distributed control systems, manufacturing execution systems and plant-wide data platforms. This provides operators and quality teams with a common view of process performance.
Role of Artificial Intelligence and Data Analytics
The volume of data generated by modern pharmaceutical plants is increasing rapidly. PAT instruments can produce large quantities of information that can be analysed using statistical tools, machine learning and artificial intelligence.
Advanced analytics can identify relationships that may not be immediately apparent through conventional monitoring. Historical process data can also be used to establish normal operating patterns and identify deviations.
Predictive models may eventually enable manufacturers to anticipate quality problems before they occur.
However, the use of AI in pharmaceutical manufacturing requires appropriate validation, data integrity, cybersecurity and regulatory oversight. The objective is not simply to collect more data, but to generate reliable, meaningful and actionable information.
Benefits Across the Manufacturing Process
PAT can be applied at numerous stages of pharmaceutical production. In raw-material handling, analytical technologies can help verify material characteristics. During granulation and blending, they can monitor moisture, composition and uniformity.
In tablet manufacturing, PAT can support monitoring of properties such as weight, hardness and content uniformity. During coating, it can provide information about coating thickness and process uniformity.
In biopharmaceutical manufacturing, PAT can be used to monitor parameters associated with cell culture, fermentation and purification processes.
The scope is therefore expanding from individual analytical applications towards an integrated approach to continuous and intelligent manufacturing.
The Future: Continuous and Adaptive Manufacturing
The long-term significance of PAT extends beyond improved monitoring. It is an important enabler of continuous pharmaceutical manufacturing.
Instead of producing discrete batches and testing them primarily after production, continuous processes can be monitored and controlled dynamically. PAT provides the real-time visibility required to maintain quality throughout the production stream.
Combined with automation, advanced analytics, digital twins and AI, PAT could ultimately create pharmaceutical manufacturing systems capable of detecting, predicting and correcting process deviations with minimal human intervention.
Conclusion
Process Analytical Technology (PAT) represents a fundamental shift in pharmaceutical quality assurance-from testing quality after manufacture to understanding and controlling quality during manufacture.
By providing real-time insight into critical process and product attributes, PAT can improve consistency, reduce variability, minimise waste and support faster decision-making. Its integration with automation, data analytics and Quality by Design principles further strengthens its potential.
As pharmaceutical manufacturing becomes increasingly connected and digital, PAT will play an increasingly important role in creating intelligent, flexible and reliable production systems.
The future of pharmaceutical quality assurance will not depend solely on testing more products; it will depend on understanding processes better. PAT provides the tools to make that transition – from reactive quality testing to proactive, predictive and ultimately intelligent quality control.